
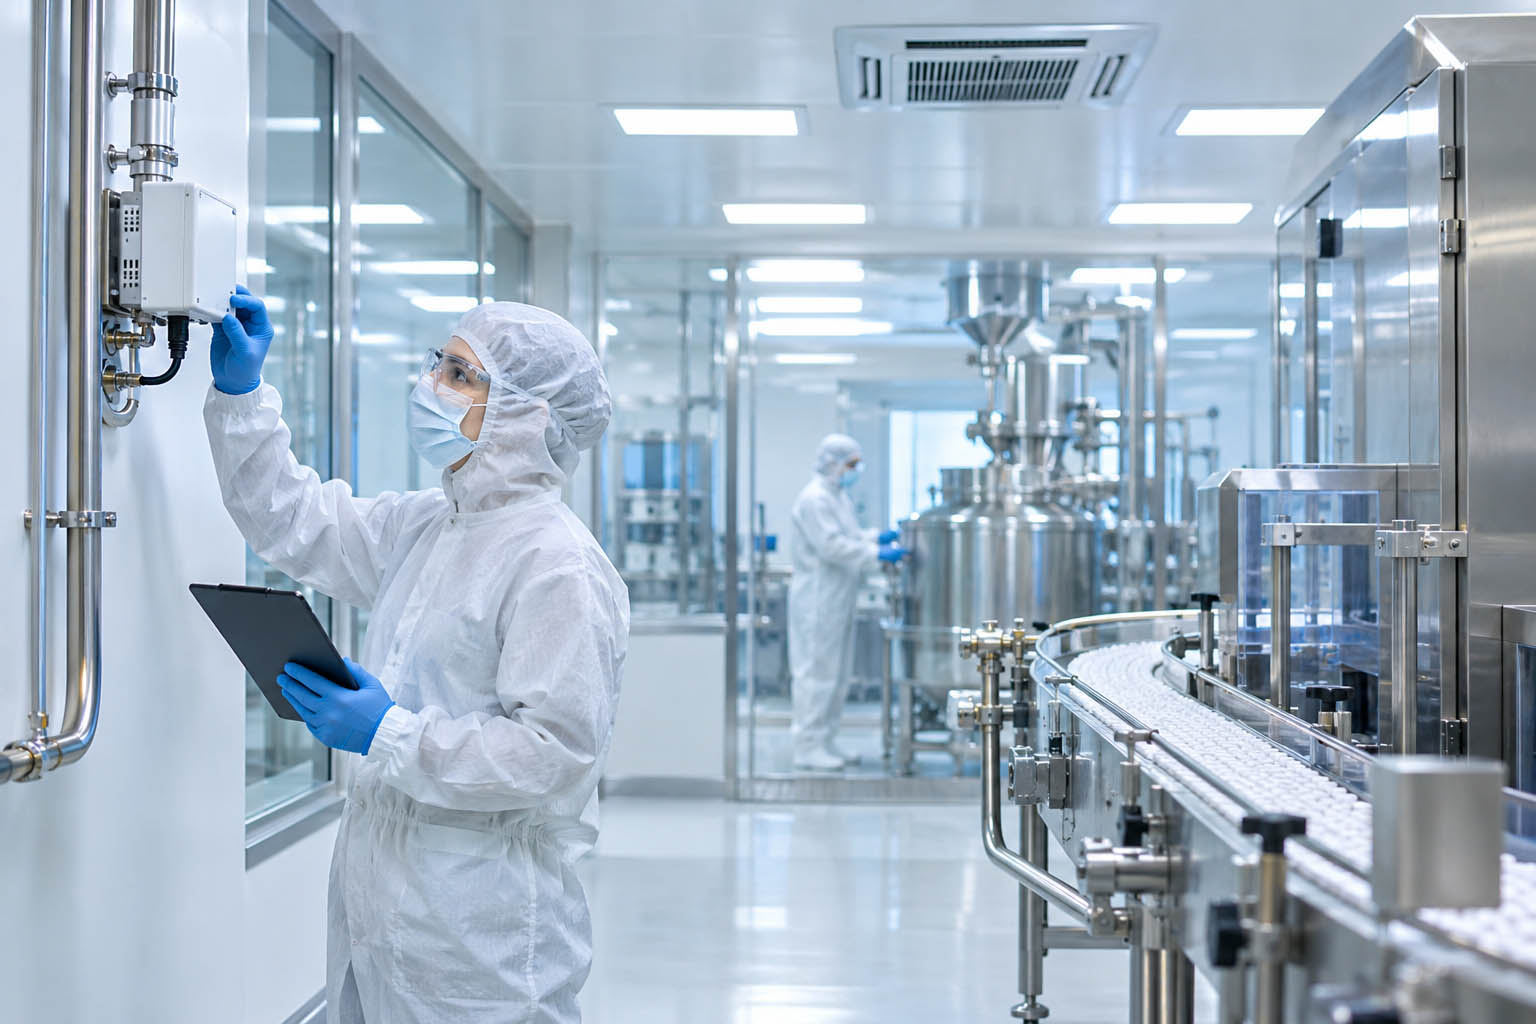
Patients rarely think about the air inside the facility where their medication was made. But the humidity in a pharmaceutical manufacturing room can affect whether a tablet dissolves correctly, whether a powder clumps during compression, or whether a coating cracks before it ever reaches a pharmacy shelf.
For doctors and health executives who track quality and safety trends across the industry, environmental control is one of the less visible factors behind drug reliability. It sits alongside sterility testing and equipment validation as part of what keeps a batch consistent from the first unit to the last.
How Moisture in the Air Affects Drug Stability
Many active pharmaceutical ingredients and excipients are hygroscopic, meaning they absorb moisture from surrounding air. Too much humidity during blending or compression can cause powders to cake, tablets to soften, or capsules to stick together during filling.
Too little humidity creates its own problems. Dry air raises static buildup, which can cause fine powders to cling unevenly to surfaces or equipment, skewing weight uniformity in a tablet batch. Manufacturers generally aim to hold rooms within a narrow relative humidity band, often in the 35 to 65 percent range, though the exact target depends on the product and process step.
Regulatory Expectations for Environmental Monitoring
The U.S. Food and Drug Administration’s current good manufacturing practice regulations require that facilities establish and follow procedures to prevent contamination and ensure product quality. In practice, this extends to control of temperature and humidity in production areas. These requirements are outlined under 21 CFR Part 211, the federal rule governing finished pharmaceuticals.
Cleanroom classification, which governs particle counts and airflow in many pharmaceutical production spaces, follows the ISO 14644 series of standards. Humidity is not part of the particle classification itself, but it directly affects particle behavior and static generation within a classified space, so facilities typically monitor both together.
The United States Pharmacopeia also addresses environmental control as part of its guidance on microbiological considerations in non-sterile manufacturing, found in USP General Chapter <1116>. Humidity above recommended ranges can support microbial growth on surfaces, which is one reason monitoring logs are reviewed during inspections.
Where Facilities Run Into Trouble
A common mistake happens when a facility treats humidity control as a single building-wide setting rather than a room-by-room specification. A compression room and a coating suite often need different target ranges, and a single central system may struggle to hit both.
Another frequent issue is condensation. Traditional steam or spray-based humidification can leave surfaces damp if droplets do not fully evaporate before settling, creating the kind of moisture pockets that encourage bacterial growth on equipment. This is part of why some facilities use systems built around self-evaporating droplets instead of larger misted particles.
Picture a mid-sized tablet manufacturer running three shifts, where a compression room drifts below 30 percent relative humidity during winter months. Static buildup starts causing powder to cling to die surfaces, leading to inconsistent tablet weight and an uptick in rejected units. The fix usually involves raising and stabilizing humidity rather than adjusting the compression equipment itself.
Equipment Choices Behind the Scenes
Facilities that need precise, surface-safe humidity control often rely on adiabatic systems that use compressed air and water to generate fine, self-evaporating droplets rather than steam or standard misting. A pharmaceutical manufacturing humidifier of this kind is designed to raise humidity within a tight range without wetting surfaces, which matters in rooms where moisture-sensitive powders and coated tablets are handled.
This is one of several engineering choices, alongside HVAC design and monitoring software, that go into keeping a production environment within validated limits. None of it replaces the core manufacturing controls required under GMP, but it supports the conditions those controls depend on.
What This Means for the Broader Industry
As pharmaceutical manufacturing continues to shift toward more complex formulations, including moisture-sensitive biologics and specialty coatings, environmental control is likely to draw more attention during facility audits. Executives overseeing plant operations may find it worth revisiting humidity logs alongside more commonly reviewed metrics like batch yield and deviation rates.
For an industry built on consistency, the air in the room turns out to be part of the formula.
